Automotive low-voltage wiring constitutes the core electrical infrastructure of 12V vehicle systems, undertaking full-vehicle power distribution, sensor signal transmission, and electronic module collaborative operation. Unlike general civil wiring design, automotive wire selection is a practical, constraint-driven engineering process. It requires comprehensive trade-offs among electrical performance, thermal derating, mechanical fatigue resistance, chemical corrosion tolerance, connector compatibility, and long-term in-vehicle reliability.
Common automotive wiring problems, such as dim lighting, intermittent sensor signals, localized overheating, and premature harness aging, can result from incorrect wire sizing, unsuitable insulation, poor terminal connections, or inadequate environmental and assembly controls. This guide explains a practical 10-step workflow for selecting automotive low-voltage wires, including voltage-drop calculations, thermal derating, insulation selection, terminal compatibility, and production verification. It is intended to support preliminary design and engineering review; final wire specifications must be validated against applicable standards and OEM requirements.
1. Automotive Low-Voltage Wire Fundamentals & Applicable Standards
1.1 Definition and Basic Application Scope
For the purposes of this guide, automotive low-voltage wiring refers primarily to conductors used in conventional 12V vehicle electrical systems. The applicable voltage limits and cable requirements must be confirmed against the relevant standard and OEM specification.
1.2 Key Standards for Automotive Wire Selection
Automotive low-voltage wire design, manufacturing, and verification follow a hierarchical standard system. Different standards govern distinct technical dimensions, avoiding cross-functional misuse. Outdated and current standard versions are strictly distinguished to ensure engineering credibility:
- ISO 19642 Series: The ISO 19642 series governs road vehicle automotive cables with divided technical scopes across individual parts. ISO 19642-1:2023 defines industry terminology and provides general design guidelines for automotive cable development. ISO 19642-2:2023 specifies standardized test methods for cable performance verification. This series does not unilaterally define wire gauge sizing, ampacity ratings, or insulation temperature grades; applicable parts, editions, and technical constraints must be verified per cable structure, conductor material, and OEM design requirements.
- SAE/USCAR-21: A performance specification dedicated to solderless wire-terminal crimp connection verification for 0–48 V DC road vehicle electrical systems, with a standard maximum ambient operating temperature of 125°C. It governs crimp mechanical strength, electrical stability, and fatigue resistance, rather than wire gauge or insulation selection specifications. For applications exceeding the standard’s defined voltage or temperature limits, OEM approval is required to validate test procedure applicability. Crimp performance verification per USCAR-21 does not replace full connector system qualification for end-vehicle deployment.
- IPC/WHMA-A-620: Defines general assembly and acceptance criteria for cable harness components. It does not specify wire cross-section standards or X-ray crimp judgment thresholds; detailed verification rules rely on supplementary OEM specifications and internal quality control plans.
- QC/T 414-2016: Effective Chinese automotive industry standard regulating wire color coding rules and model compilation methods for domestic vehicle projects.
- IATF 16949: Quality management system standard for standardized production and batch consistency control of harness products.
1.3 Conductor Material Characteristics & Application Boundaries
Automotive low-voltage wire conductors include bare copper, tinned copper, and composite materials (CCA/CCS). Material selection depends on OEM specifications, corrosion environment, crimp compatibility, and circuit safety level, rather than generalized unified rules.
Tinned copper may be specified for improved corrosion resistance where required by terminal system design and OEM specifications. Bare copper is also acceptable in low-corrosion environments per applicable standards. Final conductor plating selection depends on environmental exposure and system-level compatibility, rather than universal default rules.
CCA/CCS composite conductors offer lightweight alternatives for non-critical circuits. Compared with equivalent copper conductors, CCA and CCS display different electrical resistance, ductility, crimp behavior, and corrosion performance. Their suitability must be verified case-by-case based on conductor structure, surface treatment, terminal compatibility, circuit criticality, and formal OEM approval. They are not generic drop-in replacements for pure copper wiring.
1.4 Core Performance Requirements
Mechanical stability: Stranded conductor construction provides the flexibility required for complex automotive routing and repeated assembly bending. Long-term vibration and fatigue performance is determined by a combination of wire geometry, routing fixation, bending radius, operating temperature, and application-specific validation, rather than strand structure alone.
Thermal & chemical resistance: Automotive wire insulation is engineered to withstand continuous high-temperature exposure, engine oil splashing, coolant erosion, and dust contamination, adapting to harsh under-hood and under-body operating environments.
Electrical insulation & signal reliability: Properly specified insulation ensures stable electrical isolation and mechanical protection. System-level signal integrity additionally depends on routing layout, EMC design, and targeted shielding for high-sensitivity circuits.
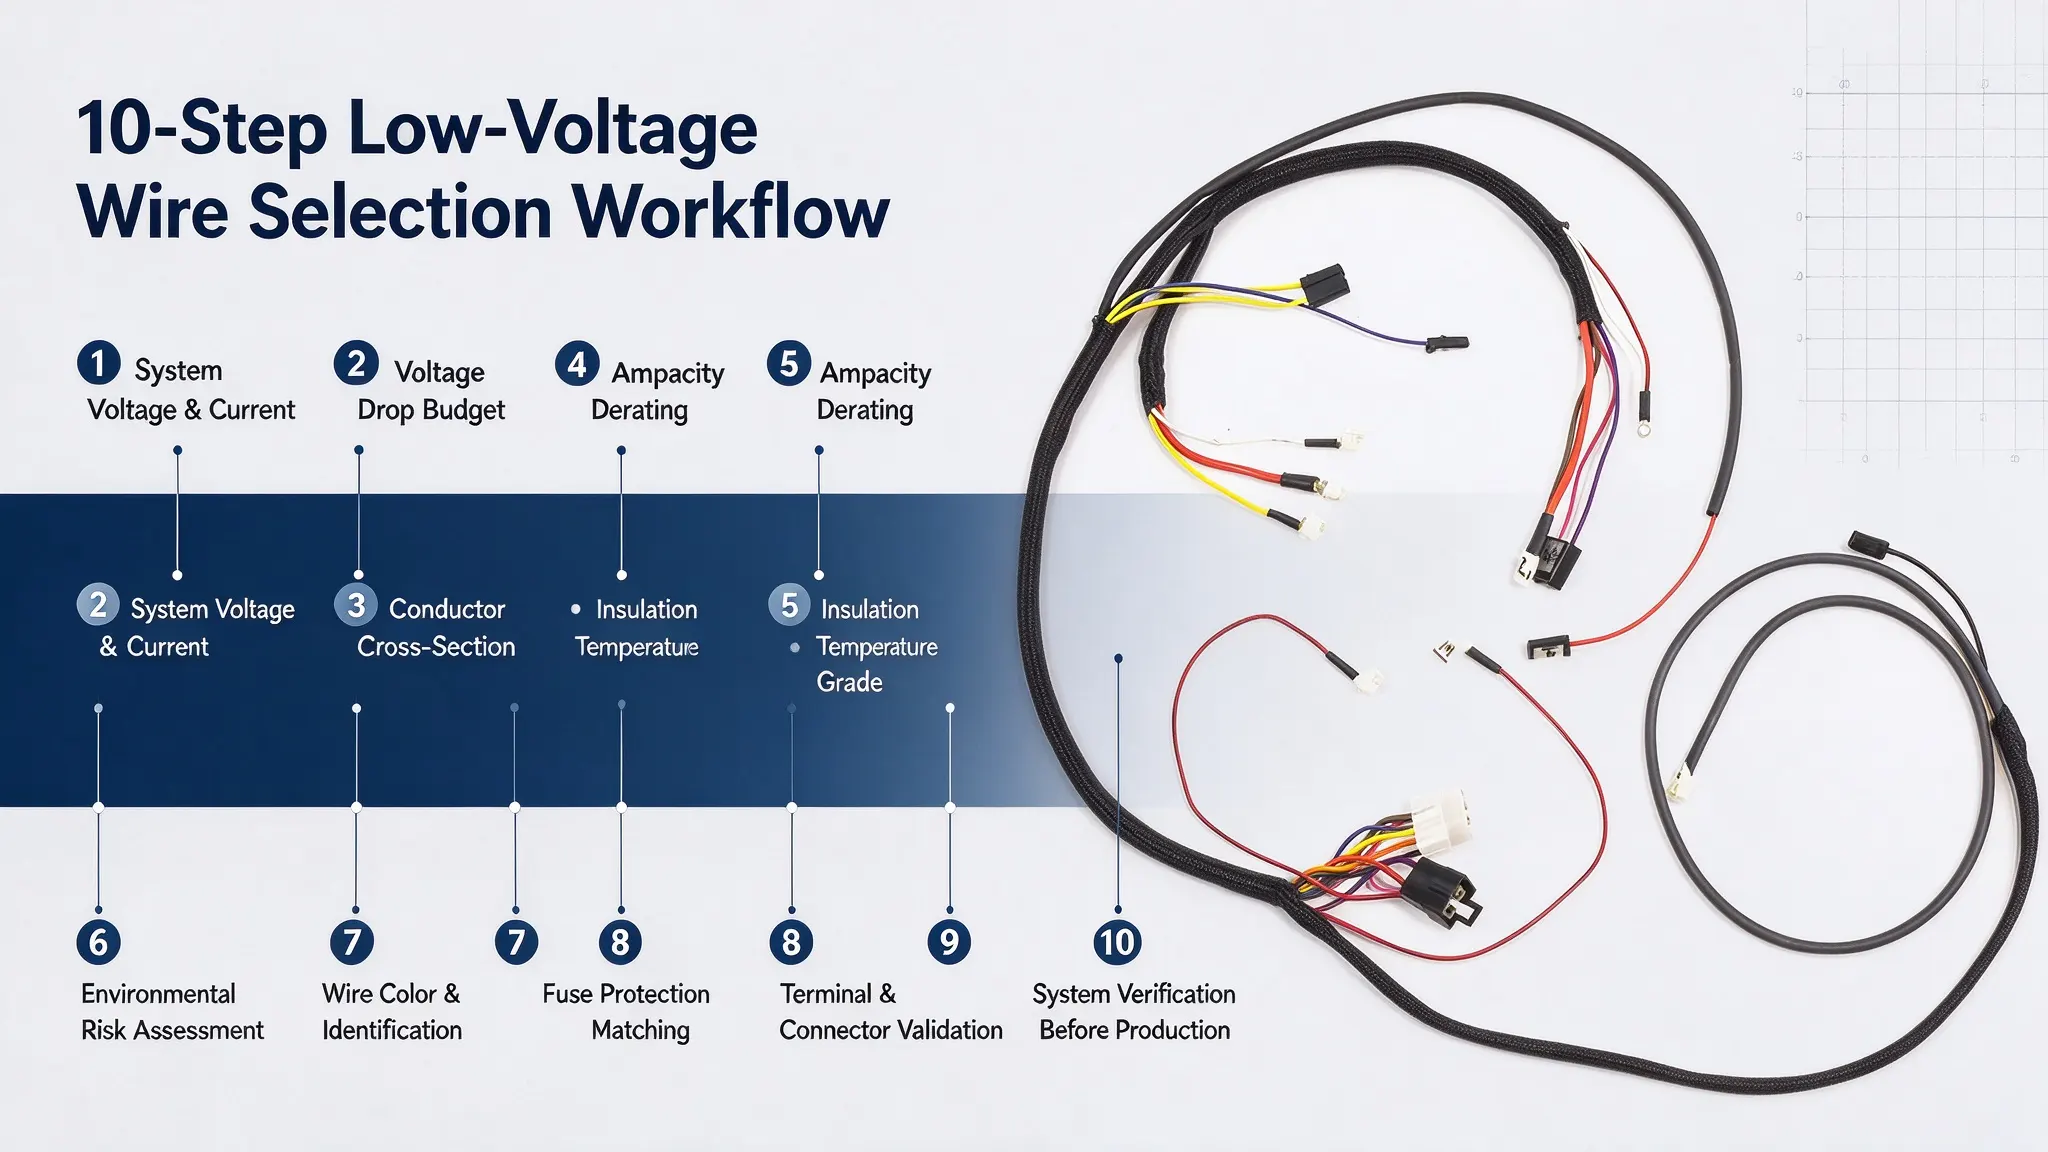
2. Standard 10-Step Low-Voltage Wire Selection Workflow (Engineering Verified)
This step-by-step workflow integrates theoretical calculation, environmental derating, mechanical verification, and production adaptability, covering the full process from preliminary sizing to mass production confirmation.
Step 1: Confirm System Voltage and Dual Load Current Parameters
Collect full electrical parameters of on-board components, clarifying continuous steady-state operating current and instantaneous inrush/peak current of each independent circuit. Both parameters serve as the basic basis for wire sizing and protection device matching.
Step 2: Define Customized Voltage Drop Budget
Calculate the total round-trip length of each circuit. A 3% voltage-drop budget may be used as an initial design target for some 12V power circuits, but it is not a universal automotive requirement. The allowable drop should be defined by circuit function, load operating limits, current profile, and OEM specifications. Signal integrity must be assessed separately where applicable.
Step 3: Preliminary Conductor Cross-Section Sizing (AWG/mm²)
Determine initial wire specifications based on load current and wiring length. AWG is mainstream in North American automotive systems, while metric cross-section (mm²) is widely used in IEC/ISO and regional markets. Specification matching must consider conductor resistance, stranded structure, insulation outer diameter, and terminal compatibility, rather than direct numerical equivalence replacement.
|
AWG Specification
|
Approximate Cross-Section (mm²)
|
Illustrative Applications (Subject to Circuit Validation)
|
|
20 AWG
|
0.52
|
Instrument indicator lights, low-current sensors
|
|
18 AWG
|
0.82
|
Body control circuits, interior lighting systems
|
|
16 AWG
|
1.31
|
Headlamps, horns, medium-current body loads
|
|
14 AWG
|
2.08
|
Window motors, wiper motors, medium-power actuators
|
|
12 AWG
|
3.31
|
Main ground circuits, generator auxiliary power circuits
|
Strict Engineering Disclaimer: The table is for preliminary reference only and cannot replace circuit-specific calculation and verification. Actual wire ampacity is affected by ambient temperature, harness bundling density, installation position, and insulation grade.
Step 4: Ampacity Derating Based on Actual Working Conditions
Standard laboratory ampacity ratings do not apply to in-vehicle conditions. Ambient heat, engine bay heat sources, and dense multi-wire bundling suppress heat dissipation and derate continuous current capacity. Thermal derating is calculated based on actual routing, wire construction, bundling density, and OEM specifications, rather than fixed zone-based rules.
Step 5: Scientific Insulation Temperature Grade Matching
Insulation temperature rating is not determined by simple installation zoning but by the maximum thermal exposure along the entire wiring path, including localized hot spots, heat exposure duration, adjacent heat sources, and OEM requirements. The temperature grade defines the continuous thermal capability of wire insulation; full system thermal reliability also depends on terminal temperature limits, crimp system performance, and harness bundling conditions. The revised scientific selection criteria are as follows:
- 105°C-rated wires: May be suitable for cabin circuits where the maximum thermal exposure, insulation system, routing conditions, and OEM requirements have been verified.
- 125°C/150°C-rated wires: Optional grades for engine compartment applications, selected based on actual maximum ambient temperature, heat radiation conditions, and formal OEM design specifications.
- 180°C-rated wires: Custom optional grades reserved for extreme local high-temperature zones, not applicable for conventional vehicle wiring scenarios.
- Cabin-engine transition wiring: Rated temperature must meet the maximum thermal requirement of the entire routing path, not simply the higher grade of two adjacent areas.
Step 6: Environmental and Mechanical Risk Assessment
Evaluate full-path risks including insulation abrasion, cyclic bending fatigue, high-humidity erosion, and chemical corrosion. Under-body harnesses prioritize wear and corrosion resistance; door/tailgate hinge wiring focuses on repeated bending fatigue resistance; high-humidity areas emphasize insulation sealing and waterproof performance.
Step 7: Standardized Wire Color and Circuit Identification
No universal global one-to-one mapping between wire color and circuit function exists. Wire color coding and circuit identification must comply with applicable OEM wiring diagrams, regional standards (e.g., QC/T 414-2016 for domestic Chinese vehicles), and project-specific specifications. Repeated colors within a single connector are permitted when supplemented by auxiliary identification methods including circuit numbers, wire marking codes, and connector cavity positioning to eliminate assembly and maintenance errors.
Step 8: Precision Fuse and Circuit Over-Current Protection Matching
Fixed empirical ratios (130%/135% fuse rating) are only preliminary references. The core protection principle is coordination between fuse time-current (I-t) characteristics and wire thermal tolerance, ensuring the fuse cuts off the circuit before insulation reaches dangerous overheating temperature. Comprehensive matching factors include wire gauge, insulation temperature grade, harness bundling state, ambient temperature, load surge current, and fault current duration. The selected fuse must also tolerate the expected normal and inrush current while providing adequate protection against fault conditions. Final coordination should be verified using the fuse time-current curve, available fault current, and the conductor's thermal withstand under the specified installation conditions.
Step 9: Terminal and Connector Compatibility Verification
Apply the applicable IPC/WHMA-A-620 acceptance criteria and OEM workmanship requirements, and validate crimp performance using SAE/USCAR-21 where applicable. Crimp microsection inspection should follow the specified evaluation criteria and control plan. Crimp verification per USCAR‑21 does not replace full connector system validation, and additional qualification testing is required for operating conditions exceeding the standard’s defined limits.
Step 10: System Verification Before Production
After completing sizing, thermal derating, and protection matching, final production verification confirms overall system compliance. This stage consolidates voltage drop performance, derated ampacity margins, fuse coordination, and mechanical/environmental durability per project validation plans and OEM requirements.
3. Core Engineering Calculations & Practical Application Case
3.1 Voltage Drop Calculation Formula
Voltage drop is the core constraint restricting long-distance wire sizing. The DC circuit calculation formula for equal positive and negative loop length is as follows:
$$\Delta V = \frac{2\rho L I}{A}$$
Parameter Definition: ΔV = total loop voltage drop; ρ = copper resistivity (0.0175 Ω·mm²/m at 20°C); L = one-way wiring length; I = continuous load current; A = conductor cross-sectional area. The formula excludes contact resistance of terminals and connectors for basic engineering estimation.
3.2 Worked Example: Voltage Drop in a 12V Circuit
Case Conditions: 12V vehicle system, 8A continuous load current, 4m one-way wiring length, 2.5mm² copper conductor, normal temperature environment
Calculation Results: Total loop length = 8m; total wire resistance ≈ 0.056Ω; actual voltage drop ≈ 0.448V; voltage drop ratio ≈ 3.73%
Engineering Analysis: The result exceeds the conventional 3% baseline. The 3% threshold is an illustrative design target rather than a universal automotive requirement. The resistivity value of 0.0175 Ω·mm²/m corresponds to conductor performance at 20°C; actual operating resistance will shift with in-vehicle working temperatures. This calculation only provides preliminary voltage drop evaluation and does not constitute a complete wire sizing conclusion. The final conductor size must also satisfy temperature-corrected resistance, derated ampacity, terminal compatibility, and protective-device coordination. A larger conductor should be evaluated against all these constraints before formal design release, rather than relying solely on voltage drop results.
3.3 Multi-Dimensional Wire Ampacity Evaluation Framework
Automotive wire ampacity cannot be determined by fixed AWG tables. The comprehensive evaluation framework covers all key engineering constraints:
|
Evaluation Dimension
|
Key Verification Content
|
|
Load Characteristics
|
Continuous current, peak surge current, working duty cycle
|
|
Electrical Performance
|
Allowable voltage drop, conductor resistance deviation
|
|
Thermal Environment
|
Maximum ambient temperature, local heat sources, harness bundling density
|
|
Wire Structure
|
Conductor cross-section, stranded structure, insulation temperature grade
|
|
Protection System
|
Fuse I-t characteristics, fault current tolerance, protection coordination
|
|
Connection System
|
Terminal crimp range matching, connector rated current capacity
|
3.4 High-Speed Signal Cable Application Boundary
CAN FD and Automotive Ethernet circuits require customized cable structures per physical-layer specifications and OEM requirements, rather than unified shielded twisted-pair design. Different high-speed interfaces have distinct requirements for pair geometry, characteristic impedance, twist pitch, and shielding schemes. This guide focuses on low-voltage power and conventional signal wiring; high-speed data cable design requires dedicated professional specification verification.
4. Typical Low-Voltage Wire Application Scenarios
4.1 Ignition and Power Distribution Systems
Low-voltage wiring supports ignition-system power supply and control signals, while the ignition system generates the required high voltage for spark discharge. Stable low-voltage power and signal transmission ensures reliable ignition triggering and full-vehicle power supply balance. Core power circuits use conductor constructions qualified for the required current capacity, voltage drop, environmental exposure, and terminal system. Bare or plated copper may be selected according to the applicable wire specification and OEM requirements.
4.2 Sensor and Intelligent Control Systems
Sensor and ADAS wiring structures depend on the interface, signal bandwidth, electromagnetic compatibility requirements, and OEM specifications. Shielded or twisted-pair constructions are used where required by the electrical interface and system-level EMC design to ensure accurate and delay-free data interaction between sensors and ECUs.
4.3 Automotive Lighting Systems
Lighting circuits are highly sensitive to voltage drop. Excessively thin wires cause excessive line loss and dim lighting; oversized wires increase harness weight and cost. Wire sizing must balance current load, wiring length, and voltage drop budget to achieve optimal comprehensive performance.
4.4 Zonal Environmental Adaptability Requirements
Engine compartment: Prioritize high temperature, oil, and flame resistance with anti-vibration fixed structures. Cockpit: Focus on flexibility, wear resistance, and low flammability for interior layout. Trunk-area: Trunk-area harnesses must meet the electrical and environmental requirements of their installation locations. Harness sections routed through tailgate or trunk-lid hinges require additional cyclic-bending and abrasion assessment.
4.5 Vehicle Ground Circuits
Ground wires provide stable current return paths and unified vehicle electrical reference potential for all electrical and electronic modules. Conductor types for safety-critical and auxiliary ground circuits are selected based on current load, environmental corrosion conditions, terminal compatibility, and official OEM design specifications, with no universal mandatory conductor type for all ground applications.
5. Industry Core Development Trends
Driven by vehicle lightweighting and intelligent upgrading, automotive low-voltage harness design continues to iterate, with three core industry development directions:
Lightweight thin-wall insulation design: Optimized conductor structures and high-performance thin-wall insulation materials reduce harness weight and improve vehicle energy efficiency while maintaining reliable electrical and mechanical performance margins.
High-density miniaturized connection: Miniature terminals and compact connectors adapt to increasingly complex on-board electrical architectures, with stricter control over routing space and assembly tolerances.
High-speed EMC optimization: Specialized shielded and twisted-pair cable structures optimize signal integrity and anti-interference performance, matching the transmission demands of intelligent driving and vehicle networking systems.
6. Production Verification & Quality Control
Modern harness manufacturing combines standardized work instructions, controlled crimping processes, appropriate inspection methods, and risk-based reliability testing to reduce process variation and improve batch consistency. Reliability testing may include thermal cycling, vibration, corrosion exposure, and other application-specific tests, as defined by the applicable product specification, OEM requirements, and validation plan. IATF 16949 supports process and quality-system control but does not, by itself, prescribe every test for every harness product.
7. Conclusion
Automotive low-voltage wire selection is a systematic engineering discipline integrating electrical calculation, environmental adaptation, structural matching, and production verification. Scientific wire sizing, graded insulation matching, and standardized protection design fundamentally improve vehicle circuit stability and driving safety.
As vehicles become lighter and more intelligent, low-voltage harness design continues advancing toward lightweighting, high-density packaging, and improved system-level EMC reliability. Our team delivers standardized, audit-ready low-voltage harness design and manufacturing solutions compliant with updated ISO, SAE, and OEM specifications, supporting customized requirements for automotive Tier 1 and OEM projects.
For professional wire selection and harness design support, please provide operating voltage, load current parameters, wiring length, working temperature range, connector specifications, and installation environment. Our engineering team will deliver targeted specification evaluation and optimized design schemes.
FAQ (High-Value Search-Oriented Questions)
Q1: What is the standard for calculating voltage drop in 12V automotive low-voltage circuits?
A: There is no universal voltage-drop limit for all 12V automotive circuits. A 3% drop may serve as an initial design target for some power circuits, but the allowable value depends on load requirements, circuit function, operating conditions, and OEM specifications. The complete circuit voltage drop should be calculated using the standard DC loop formula, accounting for conductor resistance and relevant connection resistance.
Q2: How does harness bundling and ambient temperature affect automotive wire ampacity?
A: Dense harness bundling impairs heat dissipation, while high ambient temperatures and nearby heat sources raise conductor operating temperatures, both reducing continuous wire ampacity. Derating levels are determined by wire structure, insulation rating, routing, bundling density, and OEM requirements, rather than fixed zoning rules.
Q3: How to select a reasonable insulation temperature rating for automotive wires?
A: Insulation temperature grade is defined by the maximum thermal exposure across the entire wiring path, including local hot spots and heat duration, rather than simple installation location. Transition wiring must comply with the highest thermal requirement of the full routing path.
Q4: What is the difference between AWG and mm² specifications in automotive wire selection?
A: AWG is standard for North American automotive systems, while mm² metric sizing is widely used for ISO/IEC regional applications. Similar cross-sectional values do not support direct wire replacement; conductor structure, resistance, terminal compatibility, and OEM certification must be fully verified.
Q5: What are the key criteria for matching automotive wires and crimp terminals?
A: Wire-terminal compatibility relies on matched conductor size and terminal crimp range, qualified tooling, and standardized processes. Follow IPC/WHMA-A-620 assembly criteria and OEM workmanship requirements, with SAE/USCAR-21 crimp validation applied where applicable. Crimp testing does not replace full connector system qualification.
Q6: Are CCA/CCS composite conductors applicable for automotive key circuits?
A: CCA and CCS cannot be directly substituted for pure copper automotive wires. Their applicability depends on circuit functional requirements, electrical/mechanical performance, terminal compatibility, environmental resistance, and formal OEM approval. Safety-critical circuit adoption requires dedicated validation and explicit project authorization.