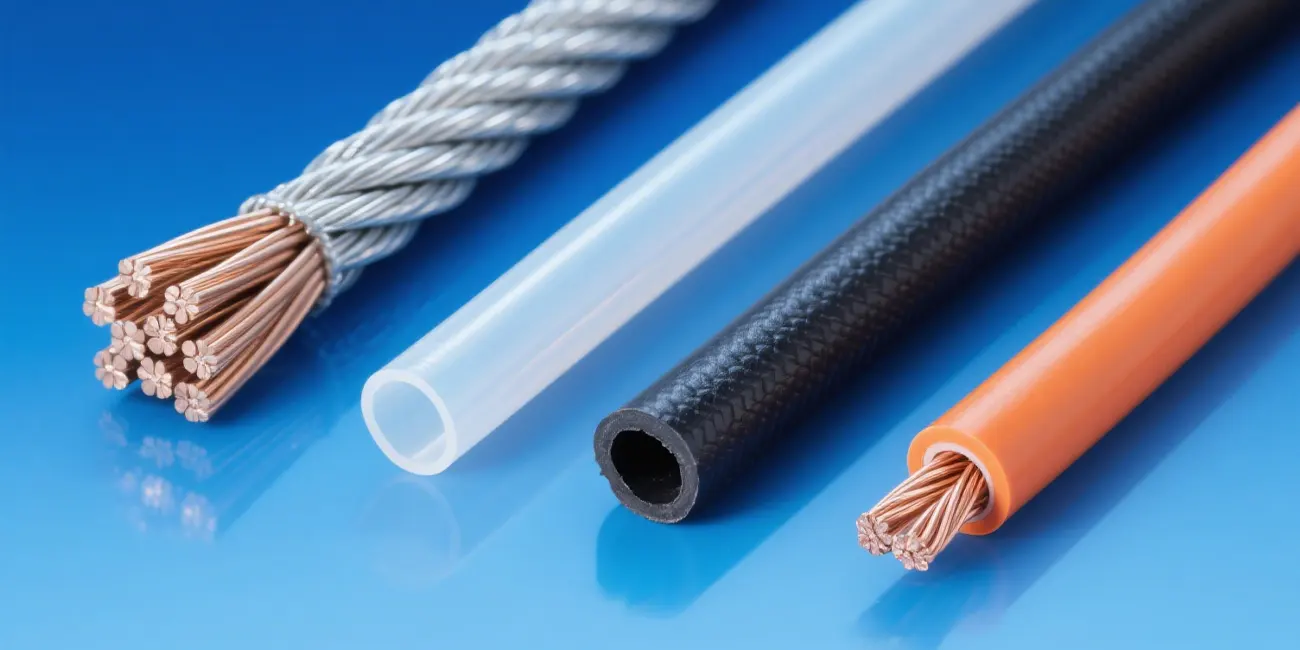
Wire harness material selection should be based on operating temperature, chemical exposure, mechanical movement, electrical performance, and regulatory standards. No single material suits all working conditions. The overall temperature rating and reliability of a wire harness are determined by the lowest-rated component in the full assembly — including insulation, jacket, terminals, connectors, and sealing structures — rather than conductor material alone. Always select conductors, insulation, shields, and outer jackets as a complete system.
The right wire harness material selection depends on five core application factors: operating temperature, chemical exposure, mechanical movement, electrical requirements, and industry regulatory standards. Every custom cable assembly requires a system-level material match to avoid premature field failure.
This practical guide breaks down targeted material selection logic for common harsh working conditions, helping OEM design engineers and procurement teams quickly confirm suitable conductor, insulation, and sheath materials for their projects.
1. High-Temperature Resistant Wire Harness Materials (Thermal Aging & Heat Resistance)
Continuous operating temperatures above 120°C easily cause insulation degradation, polymer oxidation, and sheath melting for ordinary wire harnesses, leading to short circuits and equipment failure. High-temperature-resistant wire harness configurations focus on suppressing thermal aging and maintaining stable physical and electrical performance in long-term high-heat scenarios.
Key Engineering Principle
The maximum temperature rating of a finished wire harness depends on the weakest component of the entire assembly, including insulation, sheath, terminals, connectors, and sealing materials. Upgrading conductor material alone cannot improve the overall high-temperature resistance of the harness.
Recommended Material Options
-
Conductor: Tinned copper, silver-plated copper; nickel-chromium alloy is optional for ultra-high-temperature scenarios, matched with full-system high-temperature accessories
-
Insulation: Cross-linked polyolefin (XLPE), Polyimide (PI), PTFE (excellent continuous high-temperature resistance)
-
Sheath: Fluororubber (FKM), Polyamide (PA) for superior heat aging and thermal stability
Practical Industry Solutions
Why These Materials?
XLPE delivers stable heat aging resistance and electrical insulation at mid-range high temperatures, ideal for standard automotive and industrial wiring. PI and PTFE feature exceptional thermal stability and inert properties, performing reliably under continuous ultra-high temperatures where cross-linked polymers fail. FKM and PA sheaths resist thermal oxidation, preventing sheath cracking and aging in long-term high-heat environments.
Automotive high-temperature wire constructions adopt customized cross-linked insulation systems to adapt to under-hood high-heat environments. The actual temperature grade is subject to official wire specifications and manufacturer datasheets, instead of fixed material and temperature matching. PI enameled wire and PTFE insulated wire are widely used in precision industrial and electronic equipment that requires long-term ultra-high-temperature operation.
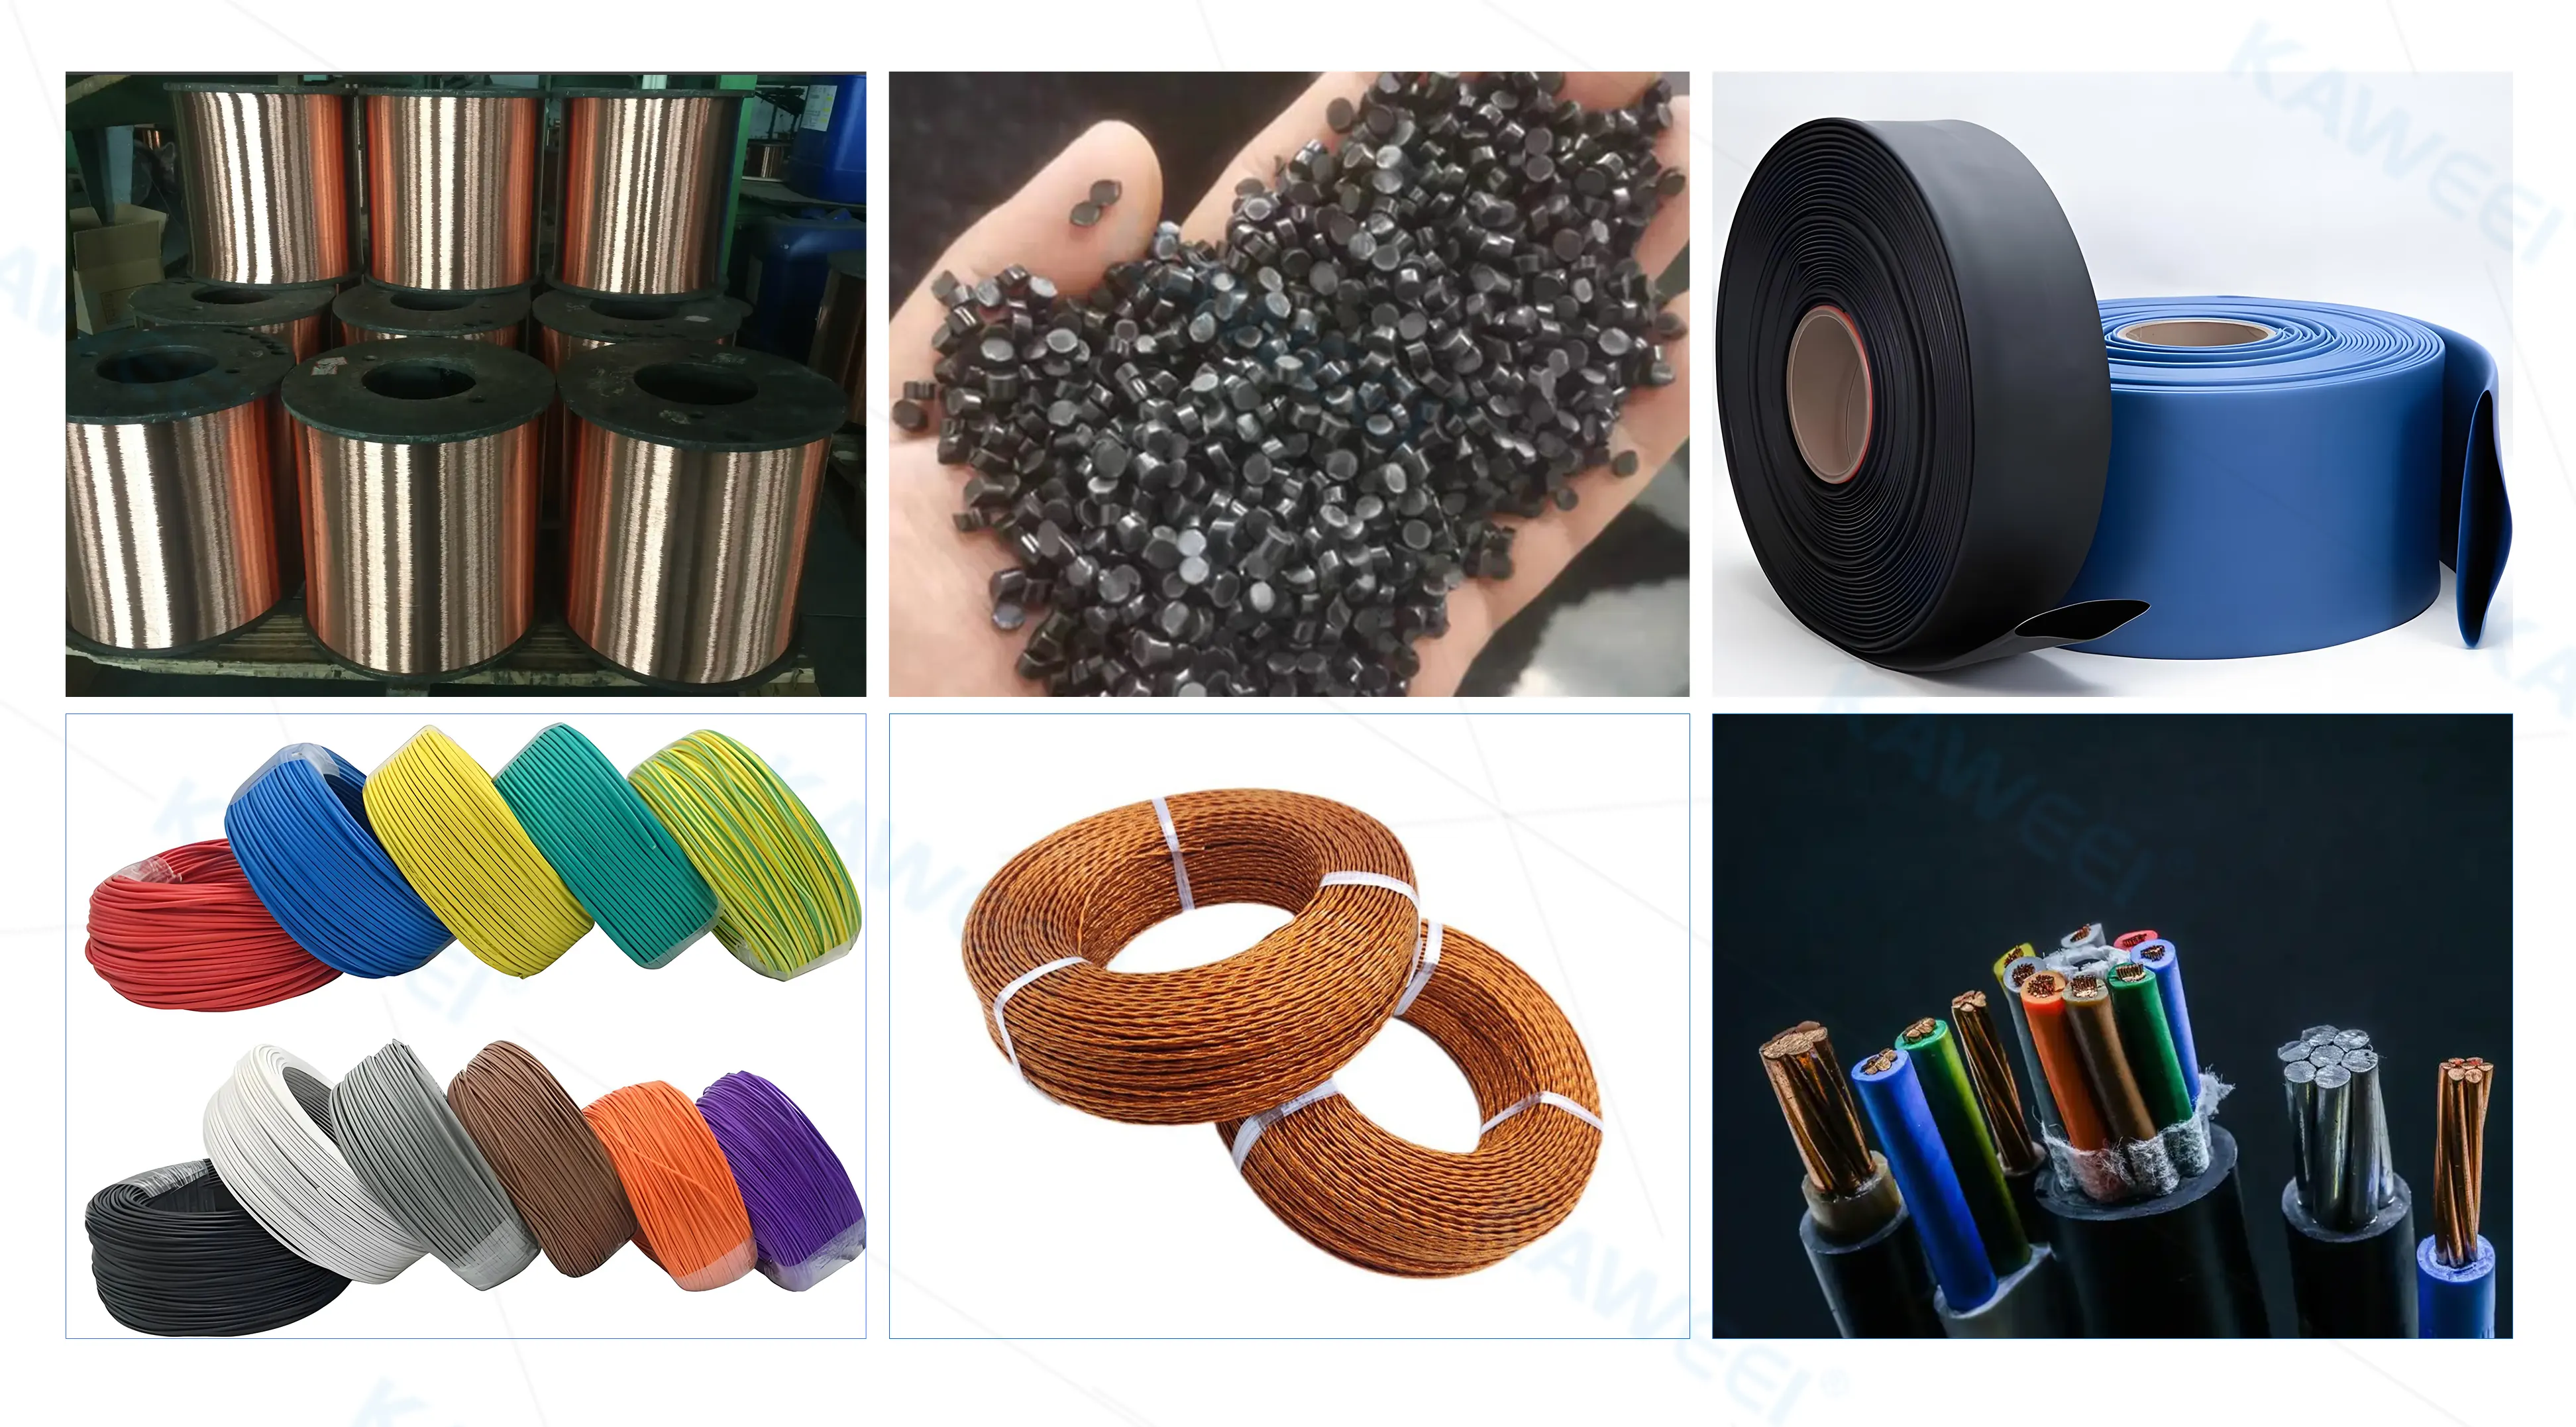
2. Low-Temperature Resistant Wire Harness Materials (Cold Flexibility & Crack Resistance)
Extreme low temperatures will harden and embrittle ordinary polymer materials, causing sheath cracking, insulation damage, and reduced conductivity during bending and vibration. Low-temperature wire harness materials must maintain stable flexibility, ductility, and electrical performance in frigid working conditions.
Recommended Material Options
-
Conductor: Soft oxygen-free copper with excellent low-temperature ductility and fatigue resistance
-
Insulation: XLPE, polyurethane (PU), silicone rubber
-
Sheath: Thermoplastic polyurethane (TPU), EPDM rubber
Practical Industry Solutions
Why These Materials?
Silicone and EPDM retain high flexibility at sub-zero temperatures without embrittlement, balancing cold resistance and weather durability. TPU and low-temperature optimized XLPE avoid cracking during repeated bending in frigid conditions, making them ideal for mobile outdoor and cold-chain equipment wiring.
Certain low-temperature-optimized PVC automotive wires can maintain basic flexibility at temperatures around −40°C, with specific performance varying by product specification and manufacturer standards. XLPE/TPU composite cables and EPDM-sheathed cables are widely used in cold-chain transportation, outdoor field equipment, and polar engineering wiring to ensure reliable low-temperature operation.
3. Chemical Resistant Wire Harness Materials (Corrosion & Fluid Resistance)
Wire harnesses used in marine, industrial manufacturing, and laboratory environments are frequently exposed to acids, alkalis, salt spray, fuel oil, and organic solvents, which easily cause sheath swelling, aging, cracking, and conductor corrosion. Chemical-resistant harnesses focus on isolating corrosive media and stabilizing structural performance.
Key Note on Material Selection
LSZH (Low Smoke Zero Halogen) materials are not designed for chemical resistance. Their core advantages are low smoke density and halogen-free flame retardancy, which reduce toxic gas and smoke emission in fire scenarios, suitable for public buildings and enclosed spaces, rather than corrosive industrial environments.
Recommended Material Options
-
Conductor: Silver-plated copper, nickel-plated copper (anti-corrosion plating layer)
-
Insulation: PTFE, ETFE (excellent solvent and acid-base resistance)
-
Sheath: FKM fluororubber, neoprene rubber
Practical Industry Solutions
Why These Materials?
PTFE and ETFE are chemically inert, resisting acids, alkalis, salt spray, and most industrial solvents with long-term stability. FKM rubber provides superior oil and fuel resistance, perfectly matching harsh engine compartment and chemical workshop operating conditions. Plated copper conductors effectively prevent electrochemical corrosion in corrosive environments.
PTFE and ETFE insulated cables resist most industrial solvents and corrosive liquids. FKM-sheathed cables are the preferred solution for engine compartments and chemical workshop equipment, effectively avoiding material aging and failure caused by long-term chemical exposure.
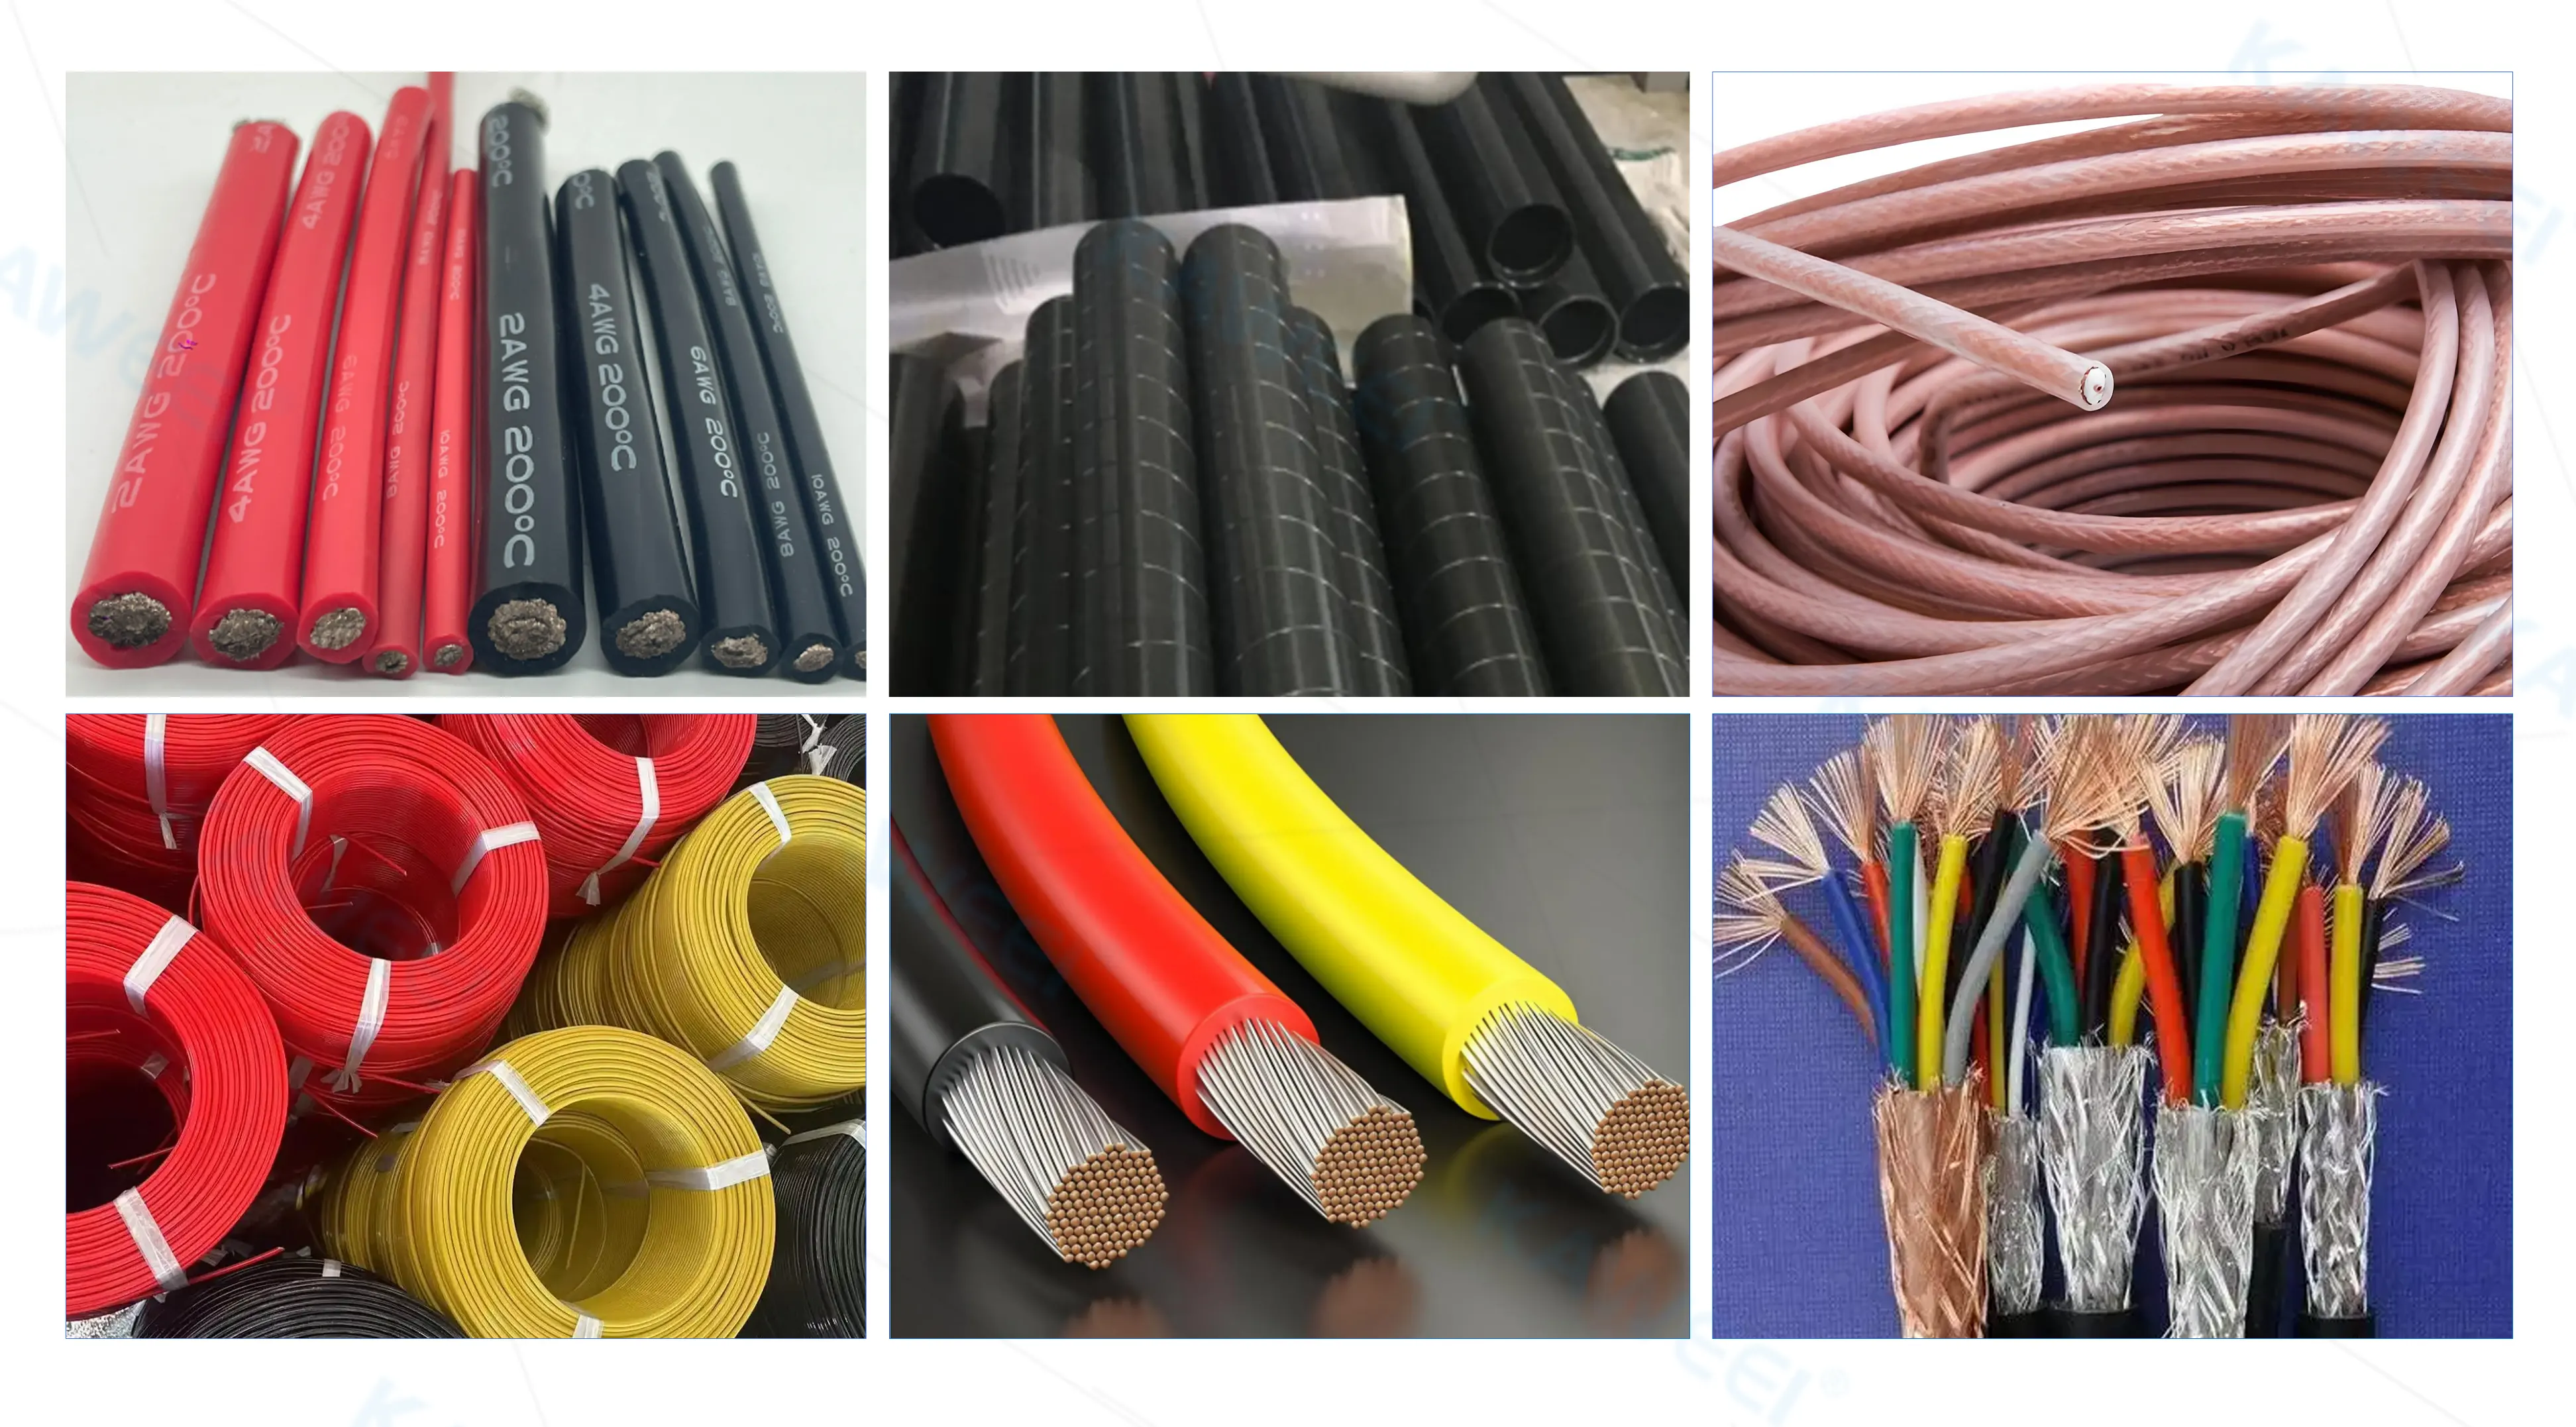
4. Mechanical Wear-Resistant Wire Harness Materials (Flex Life & Torsional Resistance)
Robotics, automated machinery, and vehicle wiring harnesses bear repeated bending, friction, vibration, and torsional motion. Mechanical-resistant harness selection cannot rely on abrasion resistance alone; flex life, minimum bend radius, and torsional resistance are core indicators for dynamic working scenarios.
Key Engineering Principle
For robotic and automated equipment applications, material selection must consider both cyclic repeated bending and multi-axis torsional motion (especially 7-axis robotic arm movement) to prevent conductor breakage and sheath fatigue failure in long-term dynamic operation.
Recommended Material Options
-
Conductor: Ultrafine stranded copper for enhanced flexibility and anti-fatigue performance
-
Insulation: Silicone rubber, PU
-
Sheath: PUR, PA, aramid-reinforced composite sheath (improves tensile and wear resistance)
Practical Industry Solutions
Why These Materials?
Ultrafine stranded copper minimizes conductor breakage under frequent bending and torsion, far more durable than solid conductors for dynamic equipment. Silicone insulation offers comprehensive flexibility for multi-axis movement, while PUR sheaths provide excellent abrasion and tear resistance. Aramid reinforcement further enhances tensile strength for heavy-duty mechanical scenarios.
Custom drag chain cables with fine-stranded copper conductors, silicone insulation, and PUR sheaths are optimized for continuous reciprocating bending and torsion. Aramid-braided reinforced cables are suitable for mining and construction machinery with high tensile and impact resistance.
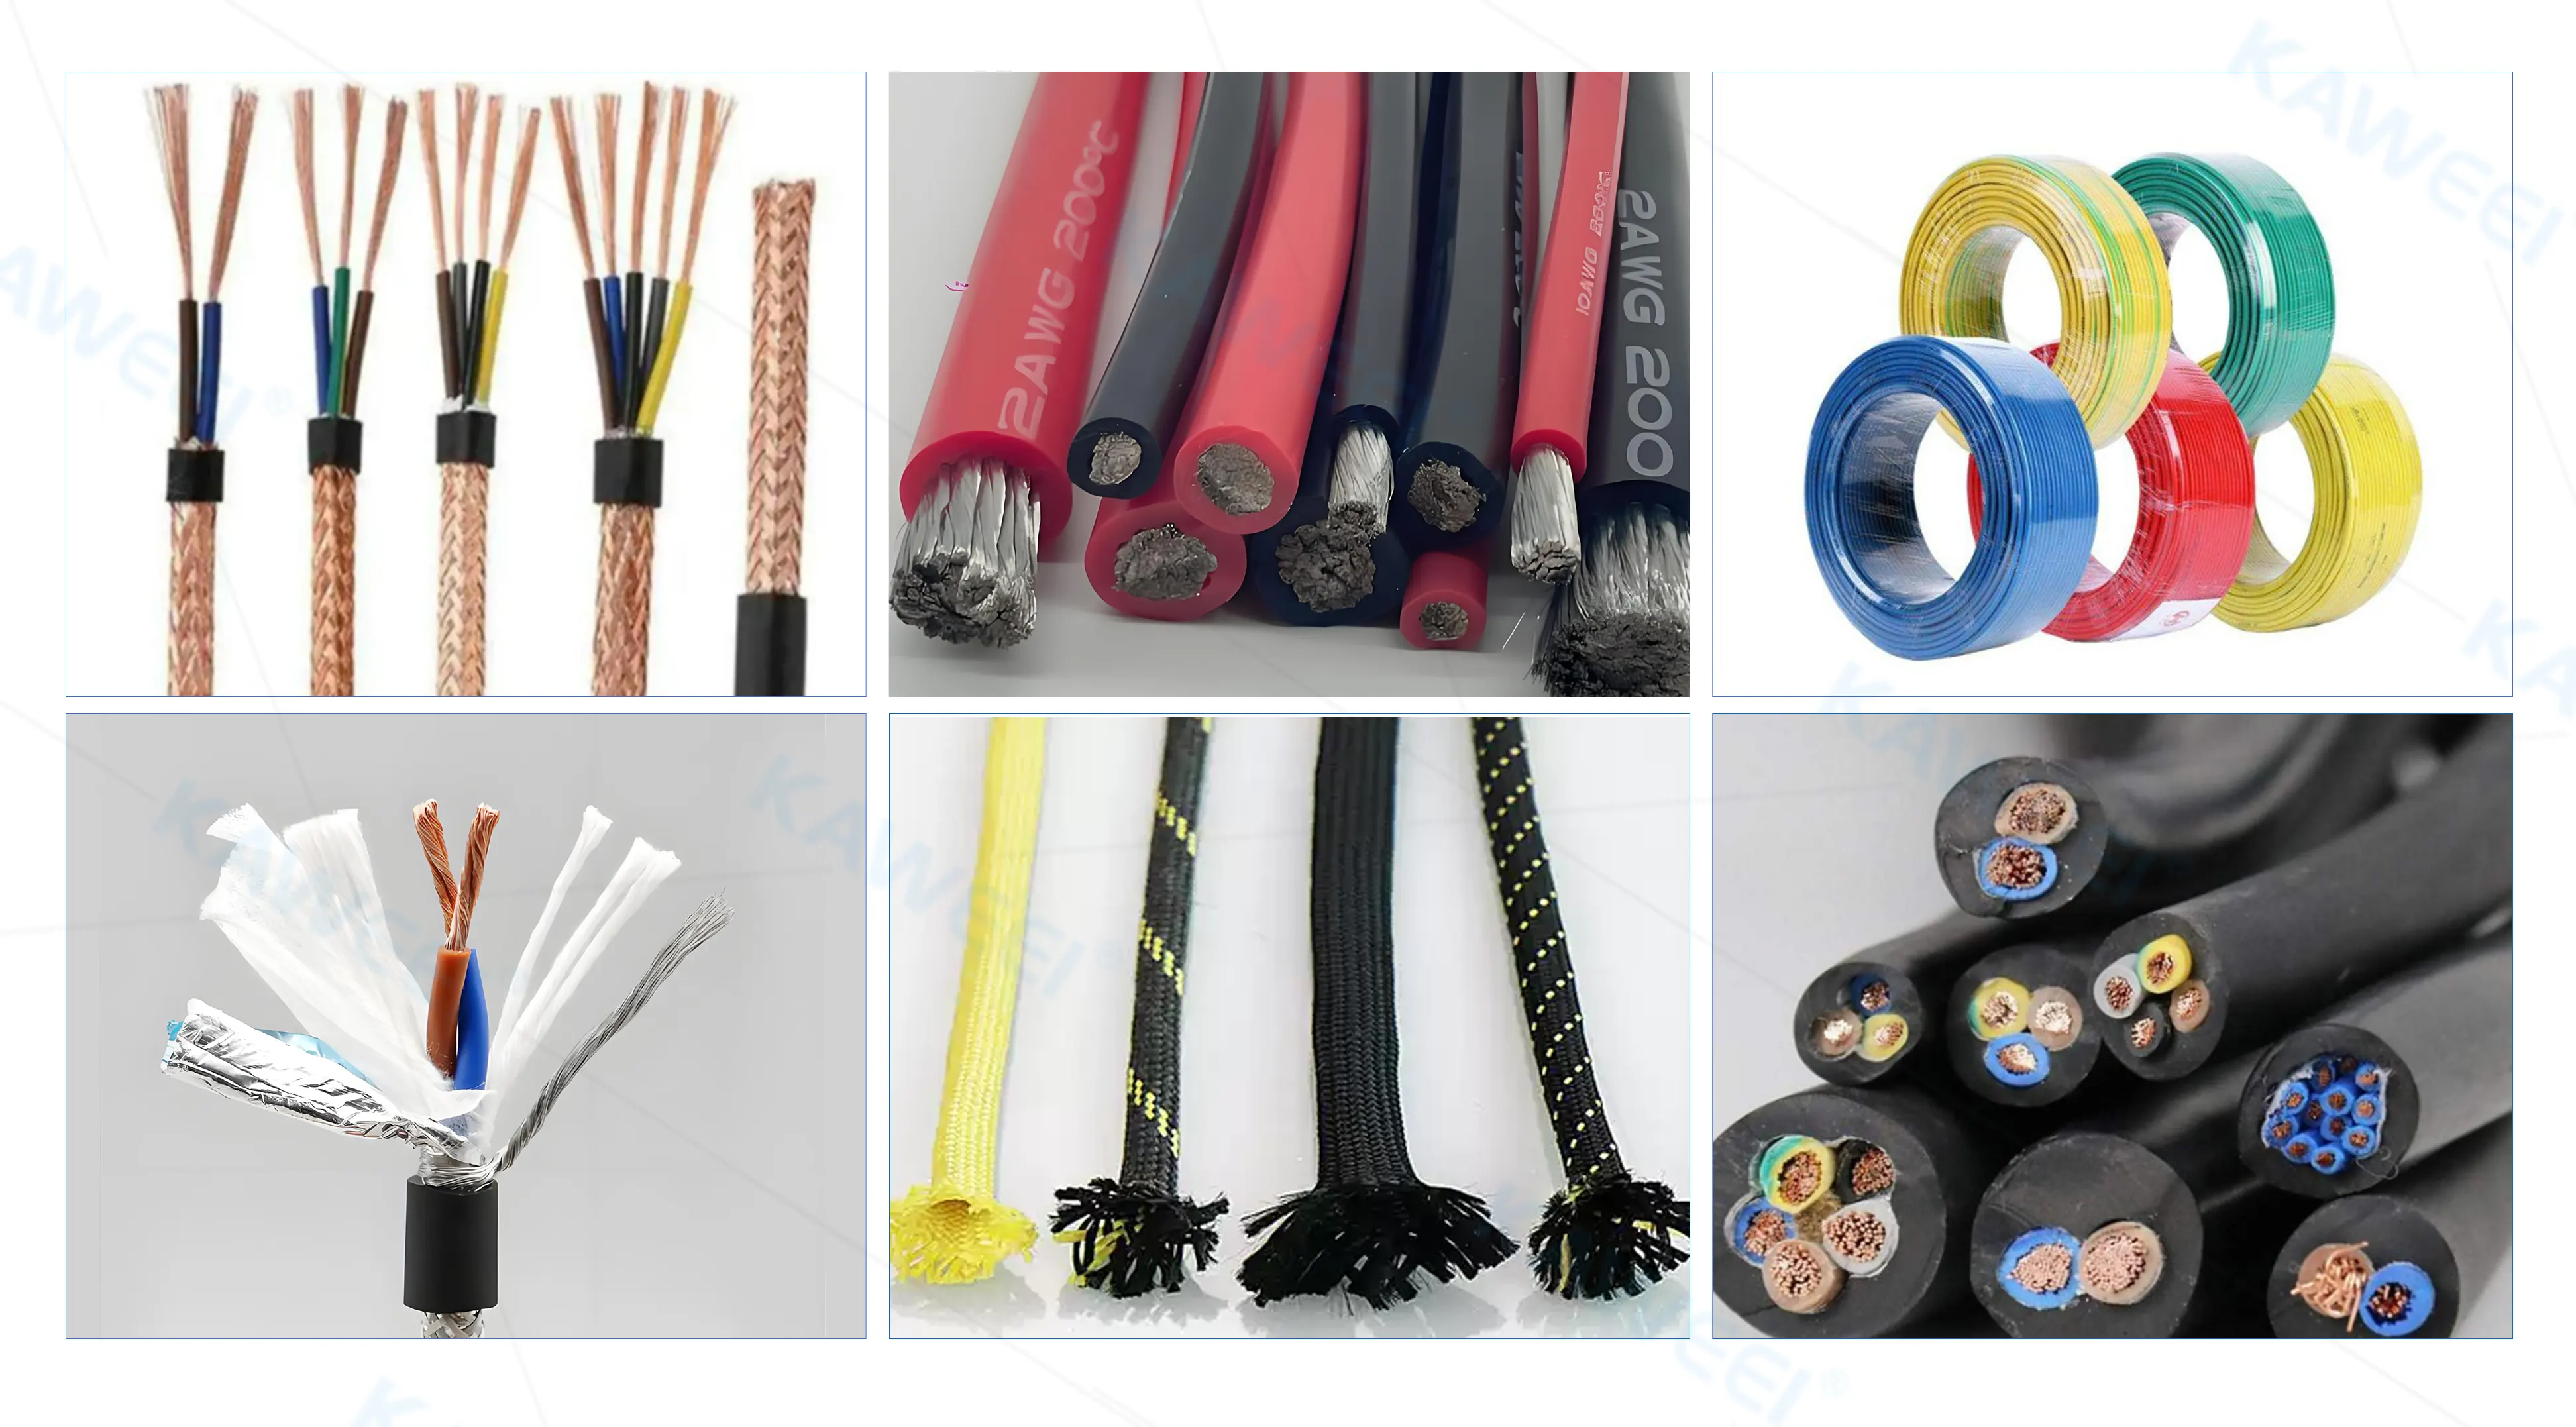
5. EMI-Shielded Wire Harness Materials (Signal Integrity & EMC Performance)
Electromagnetic interference in industrial and automotive environments causes signal distortion, data transmission loss, and equipment communication failure. EMI shielding performance depends on shielding structure, coverage, grounding design, cable geometry, and impedance control, rather than excessive copper purity.
Recommended Material & Structure Options
-
Conductor: High-quality stranded copper conductor with stable conductivity
-
Insulation: Low-dielectric-loss foamed PE, PTFE
-
Shielding: Aluminum foil single-layer shielding, copper braided shielding, foil + braid dual-layer composite shielding
Practical Industry Solutions
Why These Materials & Structures?
Low-dielectric PTFE and foamed PE insulation stabilize signal transmission and reduce interference loss. Dual-layer foil and braided shielding achieves full coverage, solving signal distortion issues caused by complex industrial and automotive electromagnetic environments. Standardized grounding and termination processes maximize EMC performance.
Dual-shielded cables with inner aluminum foil and outer copper braid adopt high-coverage shielding structures to optimize electromagnetic compatibility, effectively suppressing external EMI interference. This mature structure is widely used in automotive Ethernet, high-speed data transmission, and precision medical signal harnesses.
6. Core Wire Harness Material Performance Matrix
Use this quick comparison matrix to evaluate mainstream harness materials and select options matching your working conditions (rated by practical application performance: Excellent / Good / Moderate):
|
Material
|
Heat Resistance
|
Cold Flexibility
|
Chemical Resistance
|
Dynamic Flexibility
|
Typical Application
|
|
XLPE
|
Good
|
Good
|
Good
|
Good
|
General automotive & industrial wiring
|
|
PTFE
|
Excellent
|
Excellent
|
Excellent
|
Moderate
|
High-temperature industrial & precision electronics
|
|
Silicone
|
Excellent
|
Excellent
|
Moderate
|
Excellent
|
Robotics, medical & multi-temperature scenarios
|
|
PUR
|
Good
|
Good
|
Good
|
Excellent
|
Drag chain & dynamic motion equipment
|
|
FKM
|
Excellent
|
Good
|
Excellent
|
Moderate
|
Engine compartments & chemical exposure environments
|
7. Don’t Select Wire Harness Materials by Temperature Alone
Operating temperature is one of the most critical reference indicators, but it should never be the sole basis for material selection. A wire harness often operates in composite harsh environments. Professional material matching requires comprehensive evaluation of chemical exposure, repeated flexing cycle life, minimum bend radius, voltage and current load, EMI shielding demands, flame retardant requirements, connector temperature compatibility, and on-site installation conditions to avoid premature product failure.
8. Wire Harness Material Selection Checklist (For DFM & Quotation)
Use this checklist in the early design and DFM review stage to avoid material mismatch and on-site failure risks:
-
Maximum & minimum continuous operating temperature
-
Rated voltage, current and wire gauge requirements
-
Flexing frequency, motion type (bending / torsion / static)
-
Minimum bend radius limit
-
Exposure to oil, solvent, acid, alkali or salt spray
-
UV radiation and outdoor weather aging conditions
-
EMI shielding and signal integrity requirements
-
Flame retardancy and smoke & halogen requirements
-
Connector and terminal temperature rating matching
-
Industry regulatory compliance (RoHS, REACH, IPC/WHMA-A-620)
Need to verify conductor specifications for your design? Refer to our Wire Gauge guide and Voltage Drop Calculator to optimize circuit stability before finalizing material solutions. For customized design optimization, our team provides professional DFM review for all wire harness manufacturing and cable assembly projects.
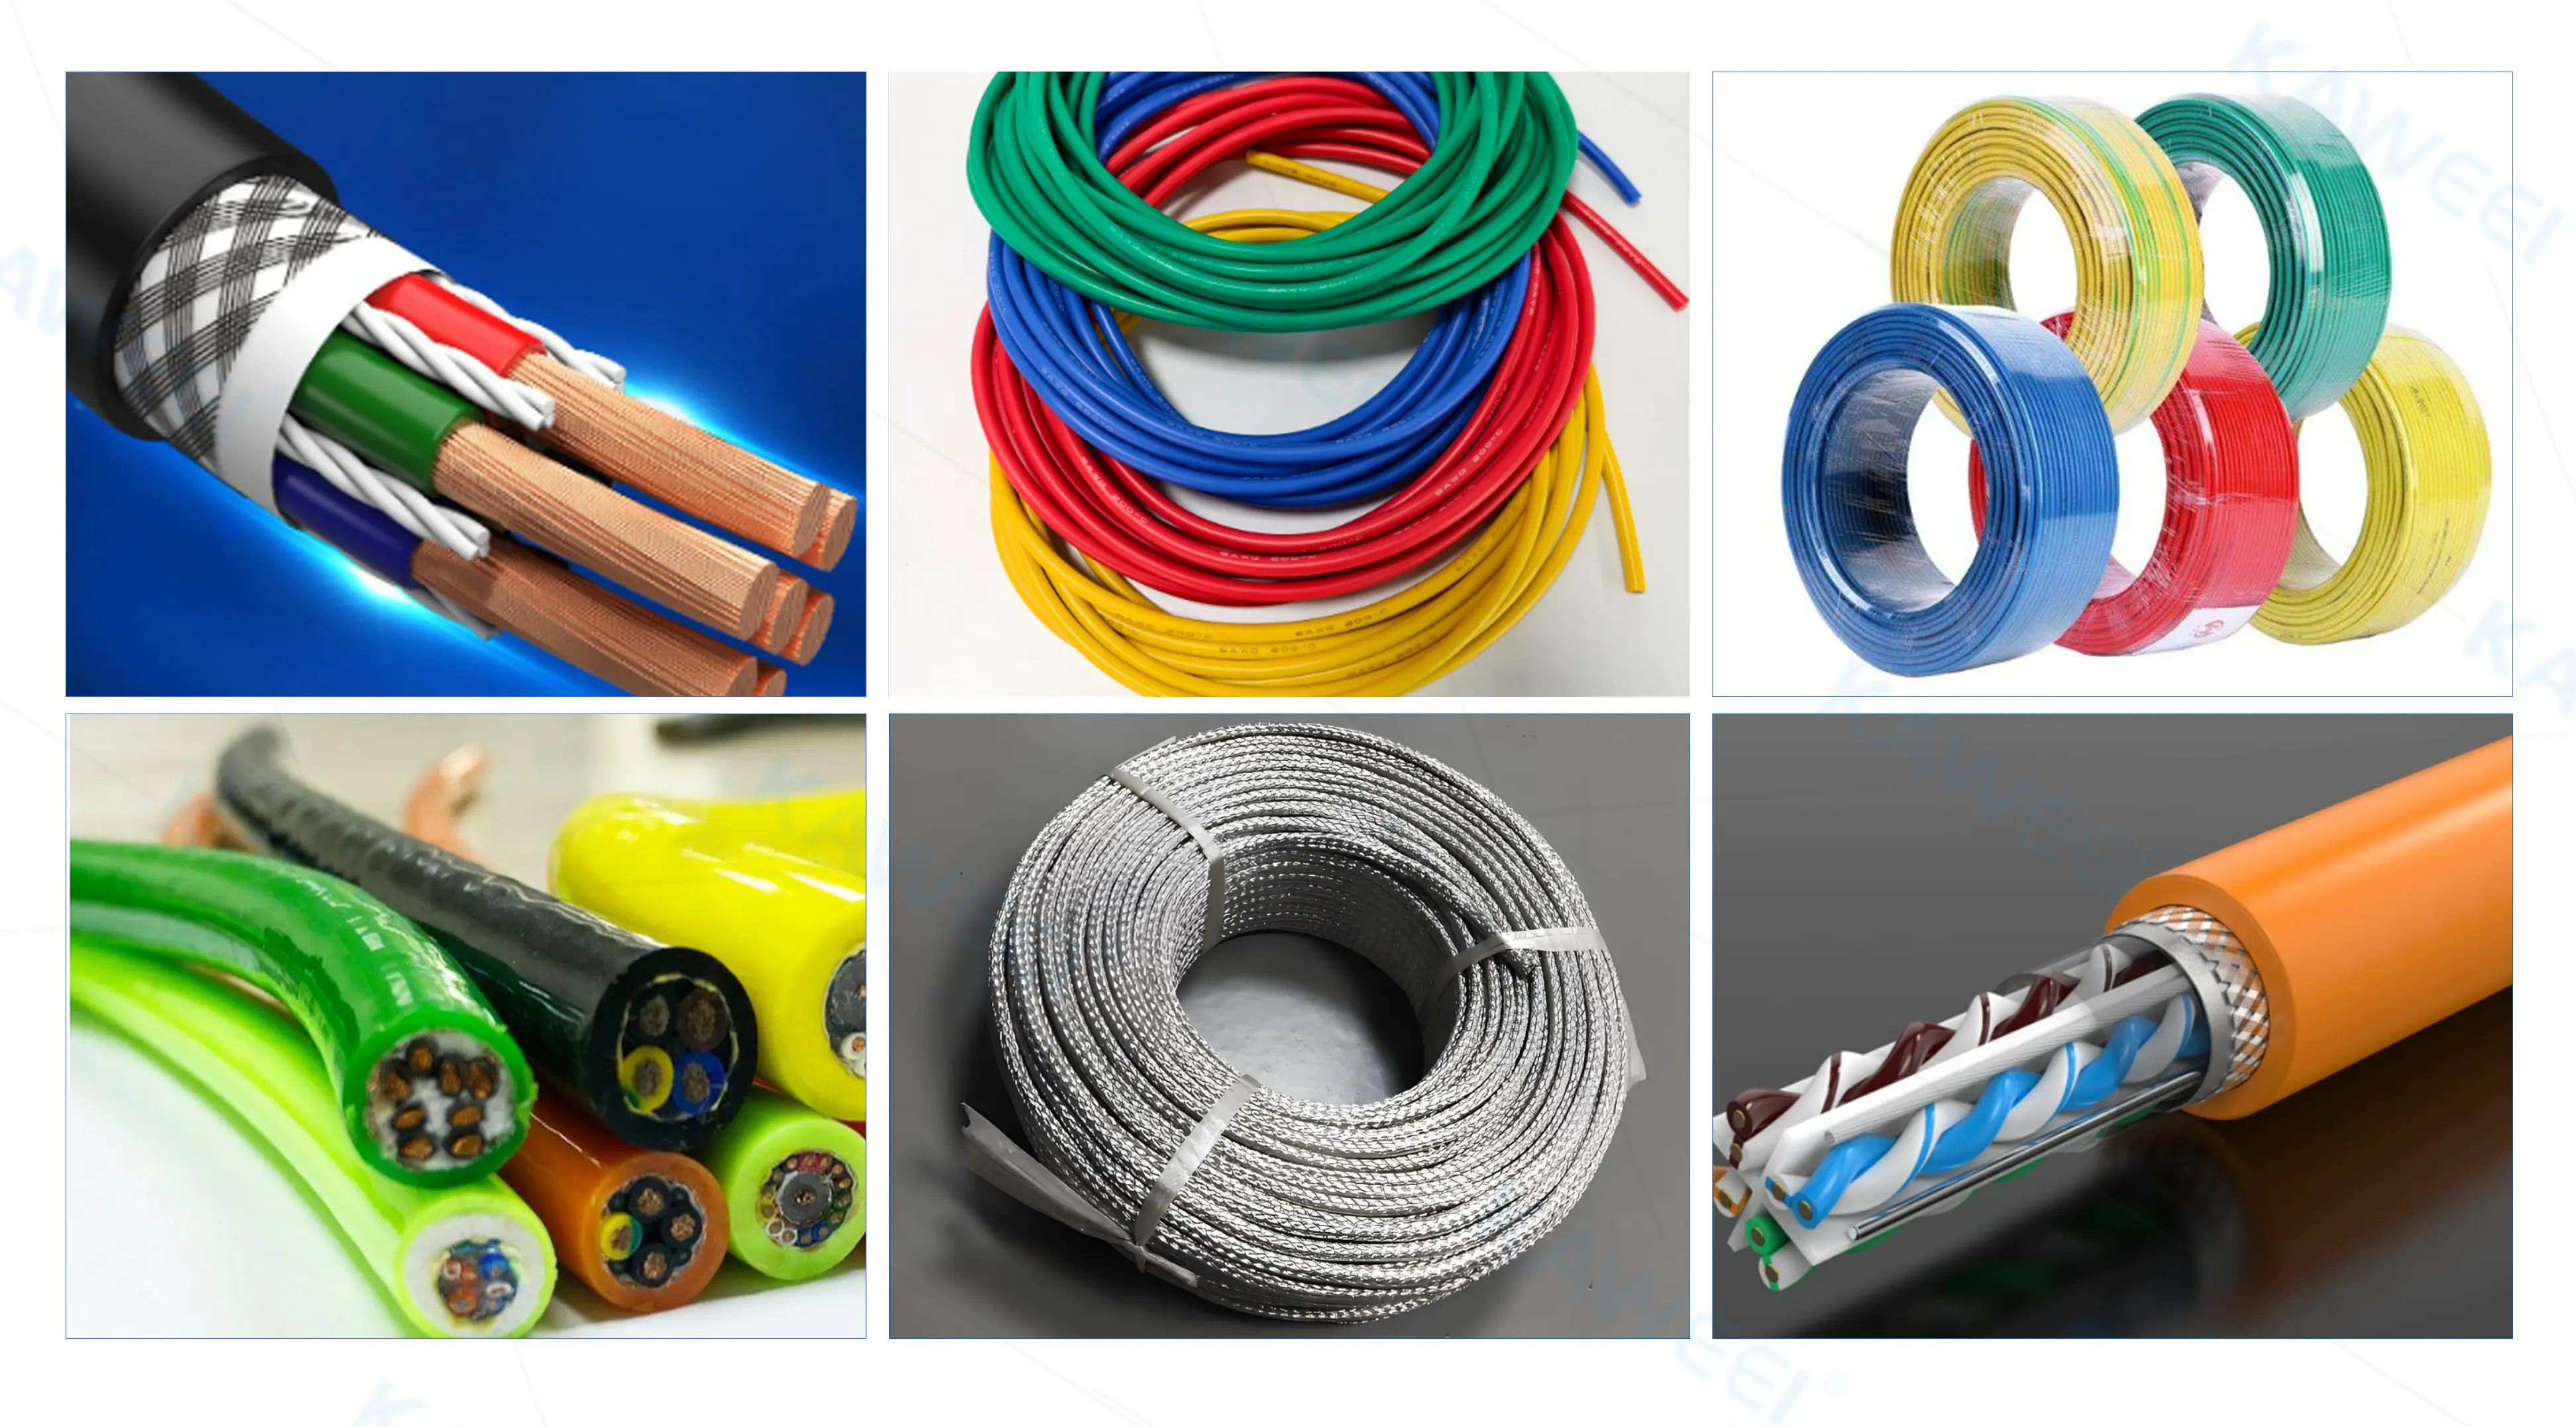
9. Final Takeaways
Professional wire harness material selection is a systematic engineering work, not a simple matching of single materials. All parameters must be matched with the actual working environment, equipment specifications, and industry standards to balance reliability, safety, and cost-effectiveness.
Kaweei is a professional custom wire harness and cable assembly manufacturer with over 12 years of OEM/ODM experience, serving automotive, industrial automation, medical devices, robotics, new energy, and communication industries. We provide one-stop services including DFM design review, rapid prototyping (24–72 hours), full-scale mass production, and strict quality testing. All products comply with IPC/WHMA-A-620, RoHS, REACH, ISO 9001, IATF 16949, and ISO 13485 standards.
Supporting prototype and low-volume customized production, we deliver stable and reliable wiring solutions for various complex harsh environments.Browse our official website for more manufacturing details, or contact our engineering team to get a free DFM review and customized solution within 24 hours.
Author: Kaweei Engineering Team | Updated: 2026 | Specialized in wire harness DFM review, custom cable assembly manufacturing, and industrial-grade wiring solution optimization
10. FAQ for Wire Harness Material Selection
Q1: Can a single wire harness material adapt to multiple harsh environments?
High-performance fluoropolymer materials such as PTFE have comprehensive high-temperature, low-temperature, and chemical resistance, but it is difficult for a single material to meet all extreme working conditions. For multi-harsh composite environments, our engineers will optimize the composite structure of insulation, sheath, and shielding layers to balance performance and cost.
Q2: Why cannot conductor material alone improve the harness temperature resistance?
The conductor itself has excellent temperature resistance, but insulation, sheath, terminals, and sealing materials will age and fail first under high temperature. The overall temperature grade of the finished harness is determined by the weakest component of the entire assembly system.
Q3: What is the core of EMI shielding harness design?
EMI shielding effect mainly depends on shielding structure coverage, grounding termination process, cable pair twisting, impedance matching, and installation environment. Excessively high copper purity cannot effectively improve anti-interference performance; standardized structural design and processing technology are the key.
Q4: How do I choose between PTFE, silicone, XLPE, and PUR?
Select materials based on your core operating demands: ChooseXLPE for cost-effective general industrial and automotive static wiring;PTFE for ultra-high temperature and heavy chemical exposure scenarios;silicone for robotics, medical equipment, and multi-temperature flexible scenarios; PUR for dynamic drag chain equipment requiring long flex life and abrasion resistance.
Q5: What information should I provide when requesting a custom wire harness quote?
To obtain an accurate DFM review and formal quote, provide core parameters including: operating temperature range, working environment (chemical/corrosion/flexing), voltage/current ratings, wire gauge specifications, minimum bend radius, shielding and flame retardant requirements, connector models, and applicable industry compliance standards. Full parameter support helps our engineers optimize material matching and control project cost.